


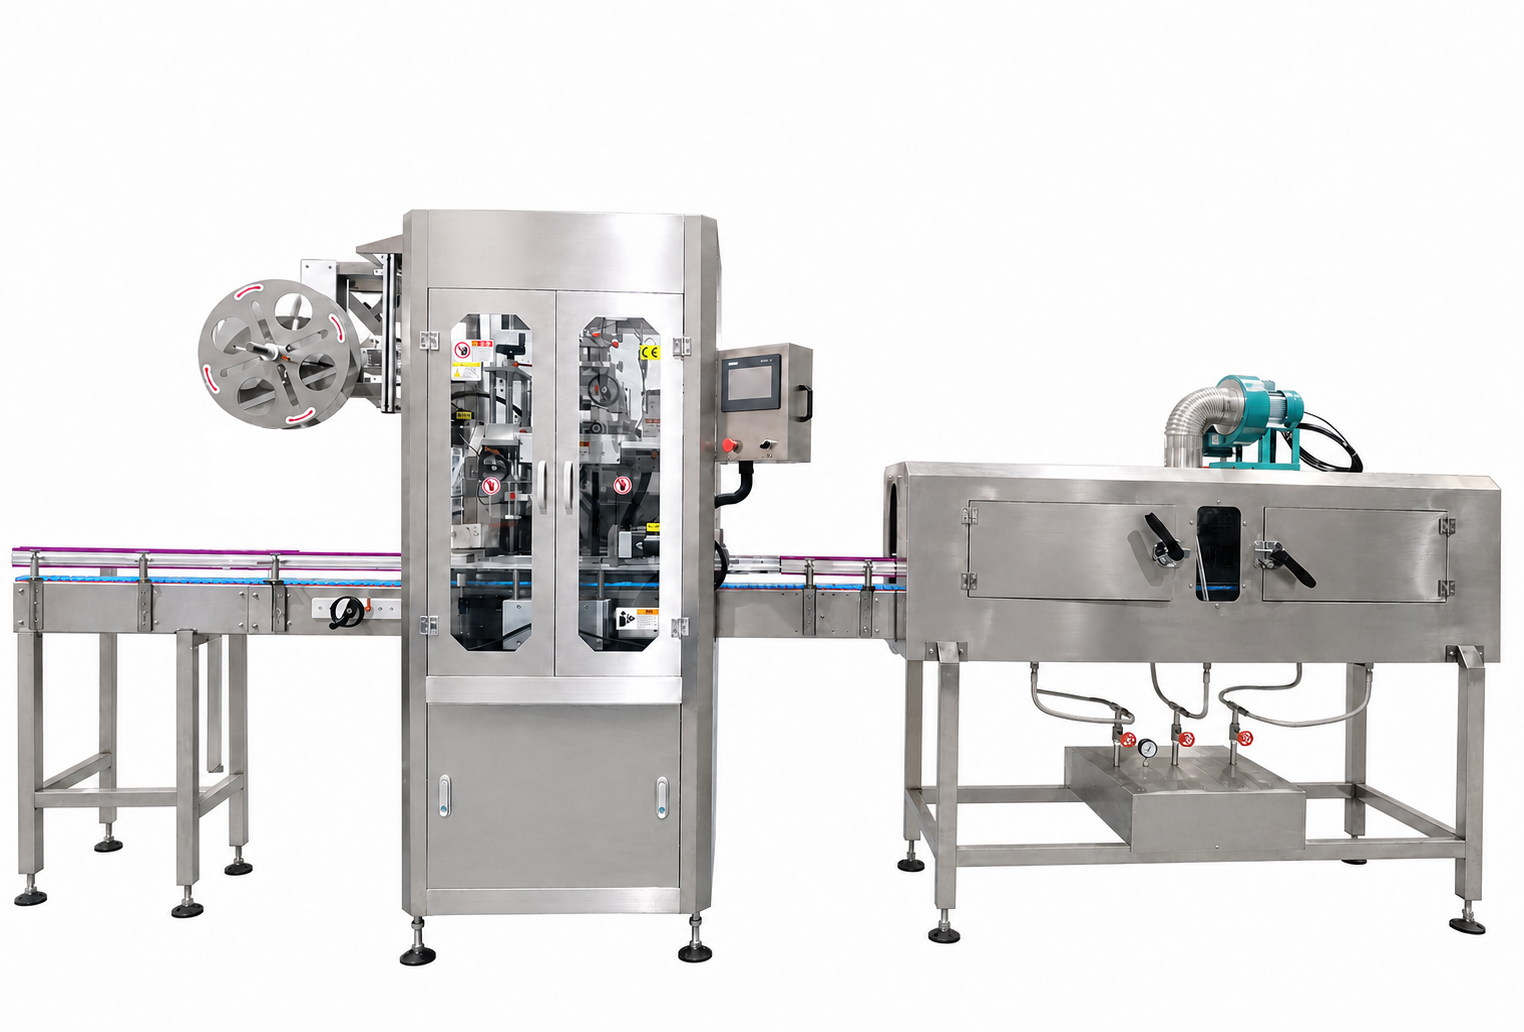
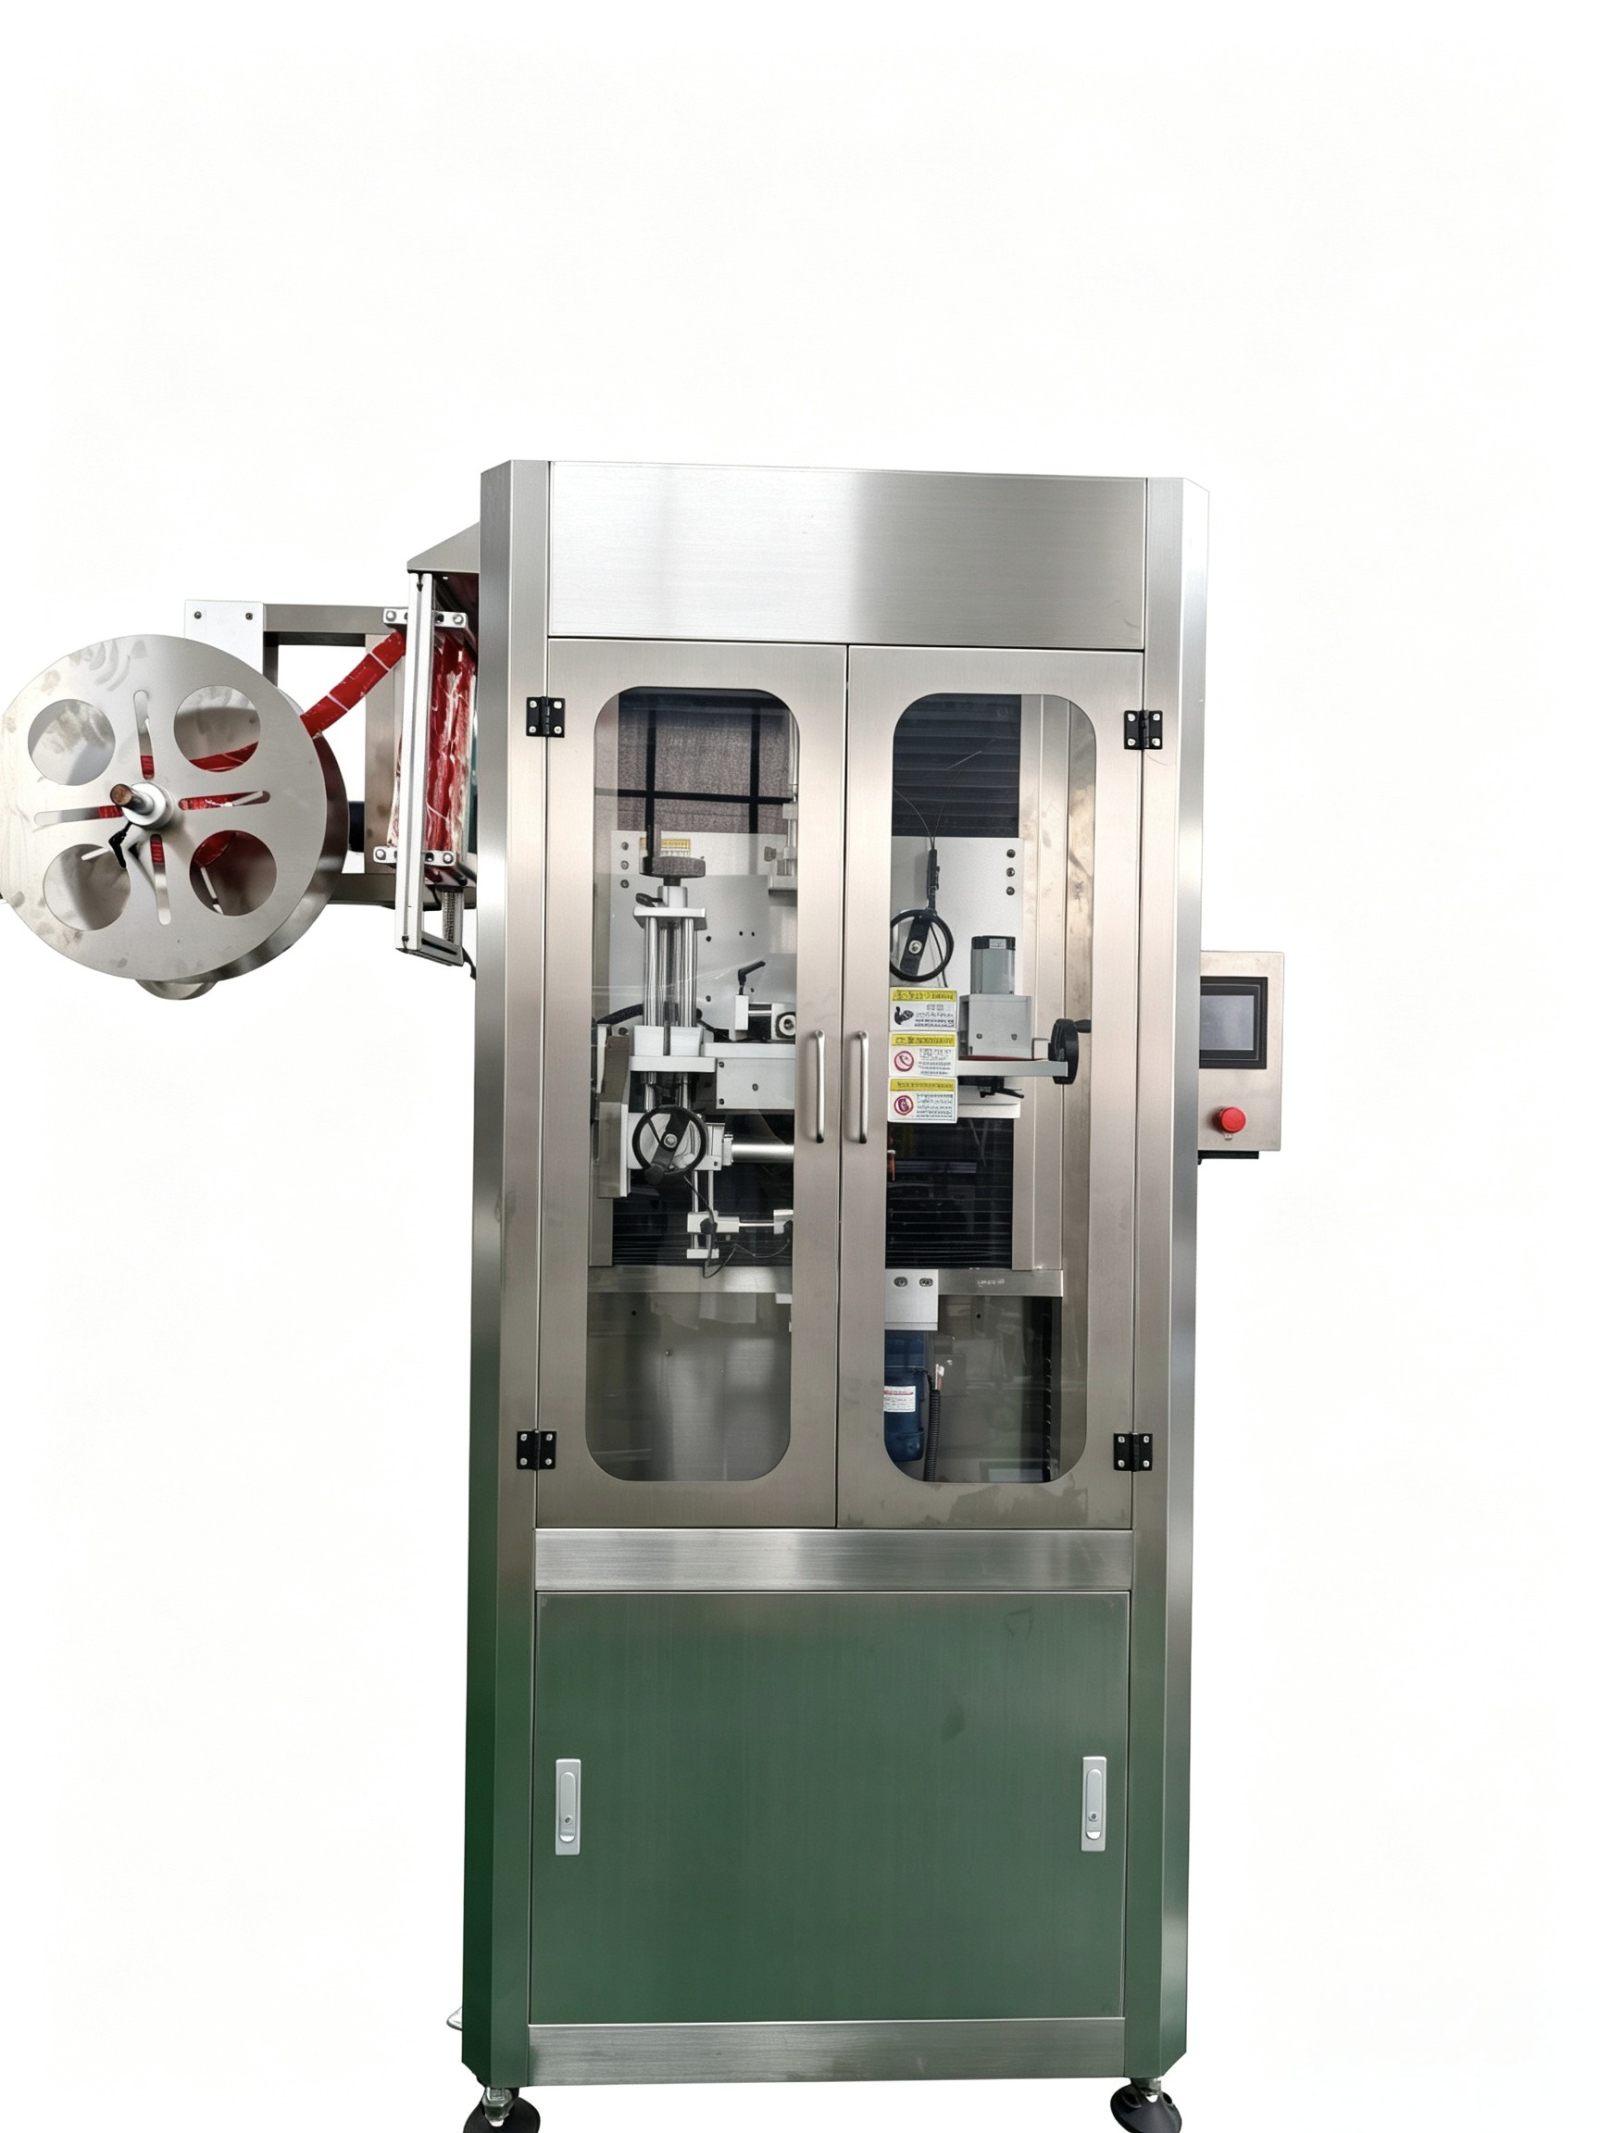
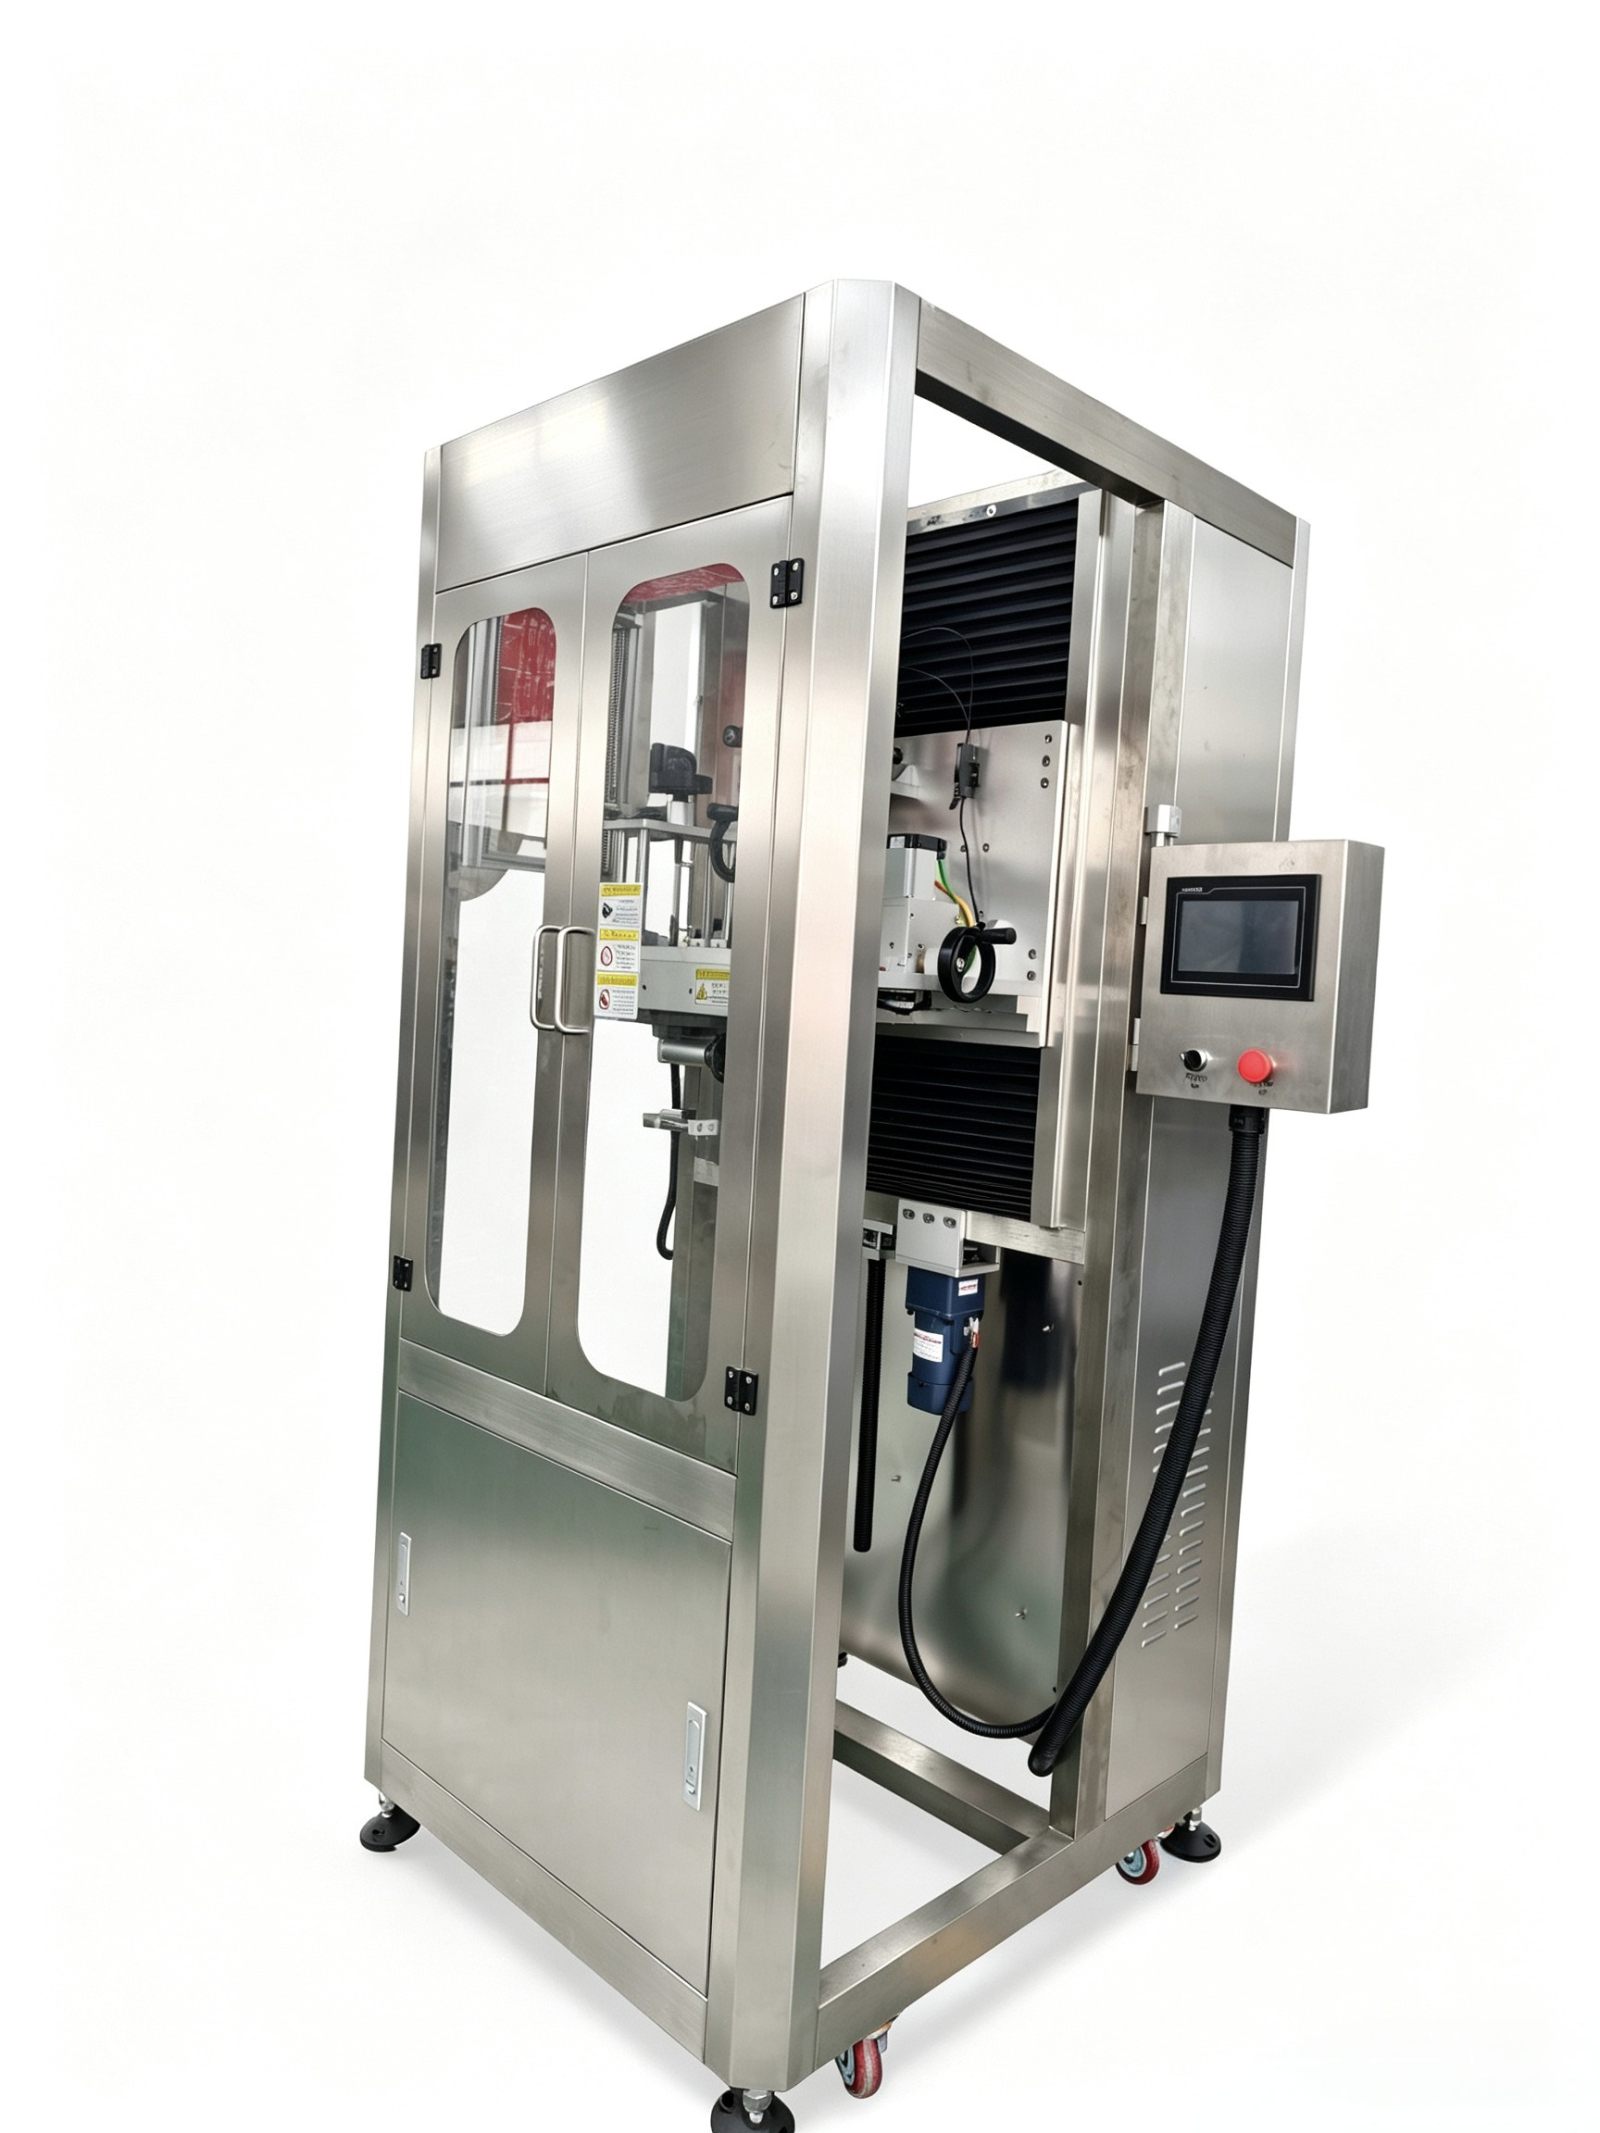
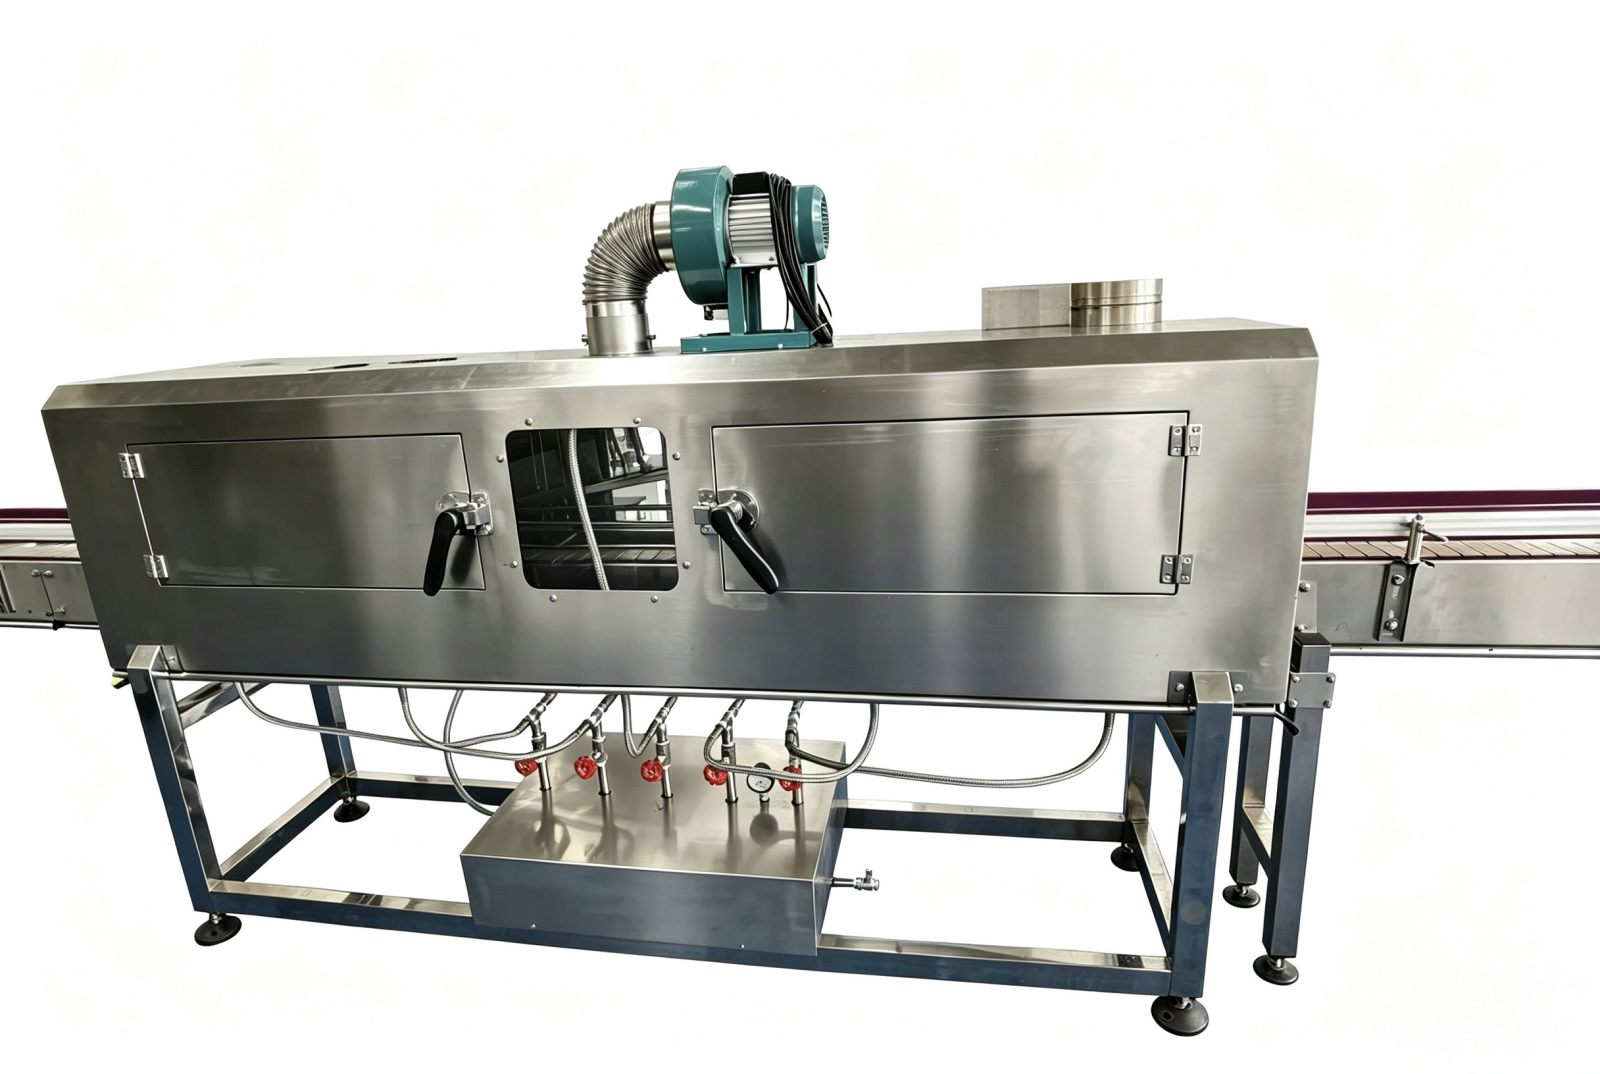
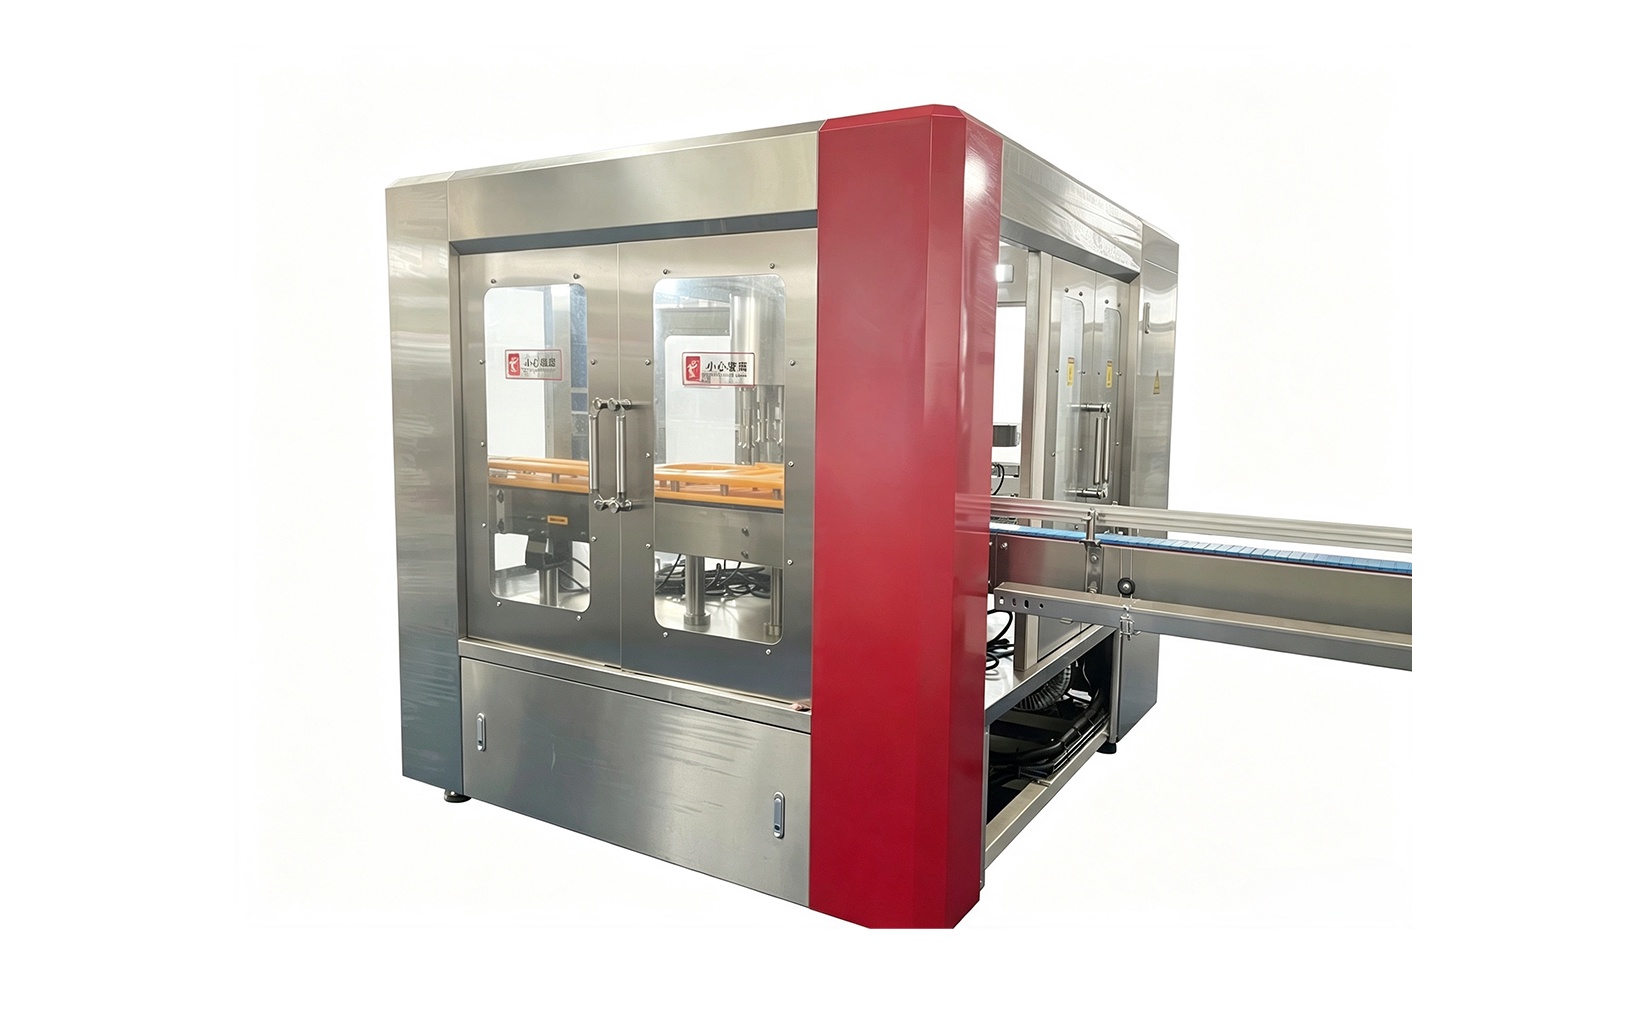
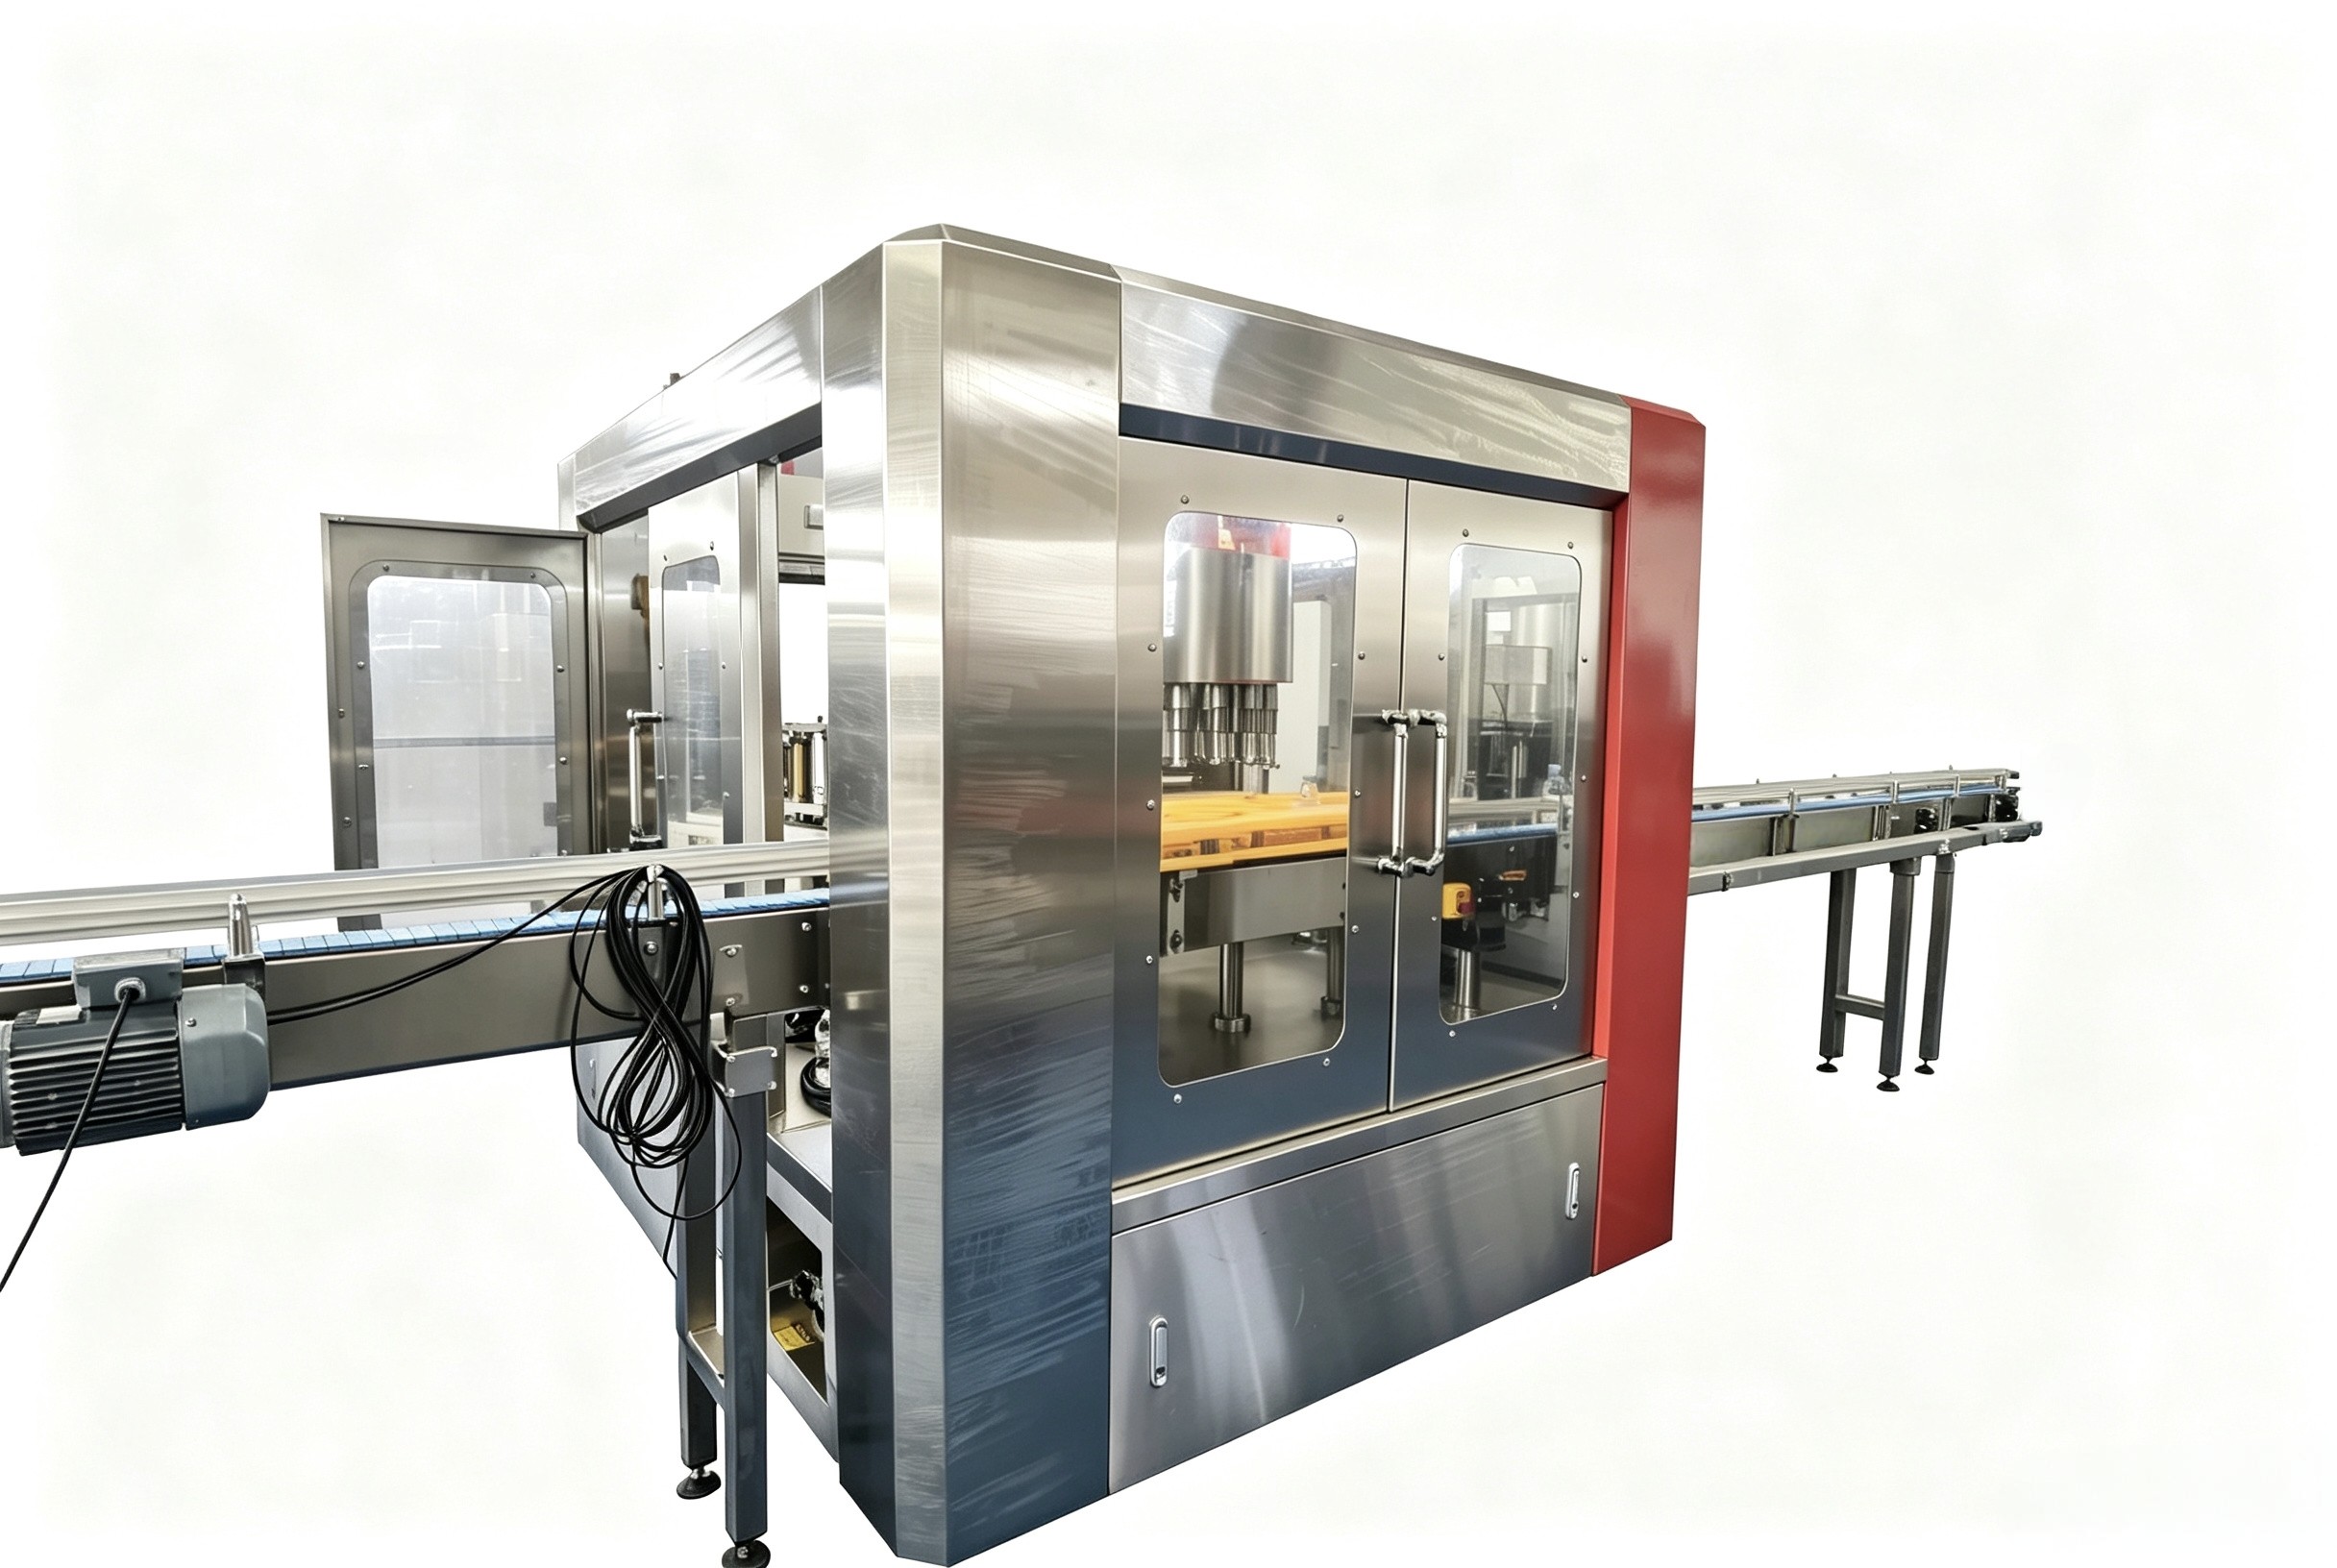
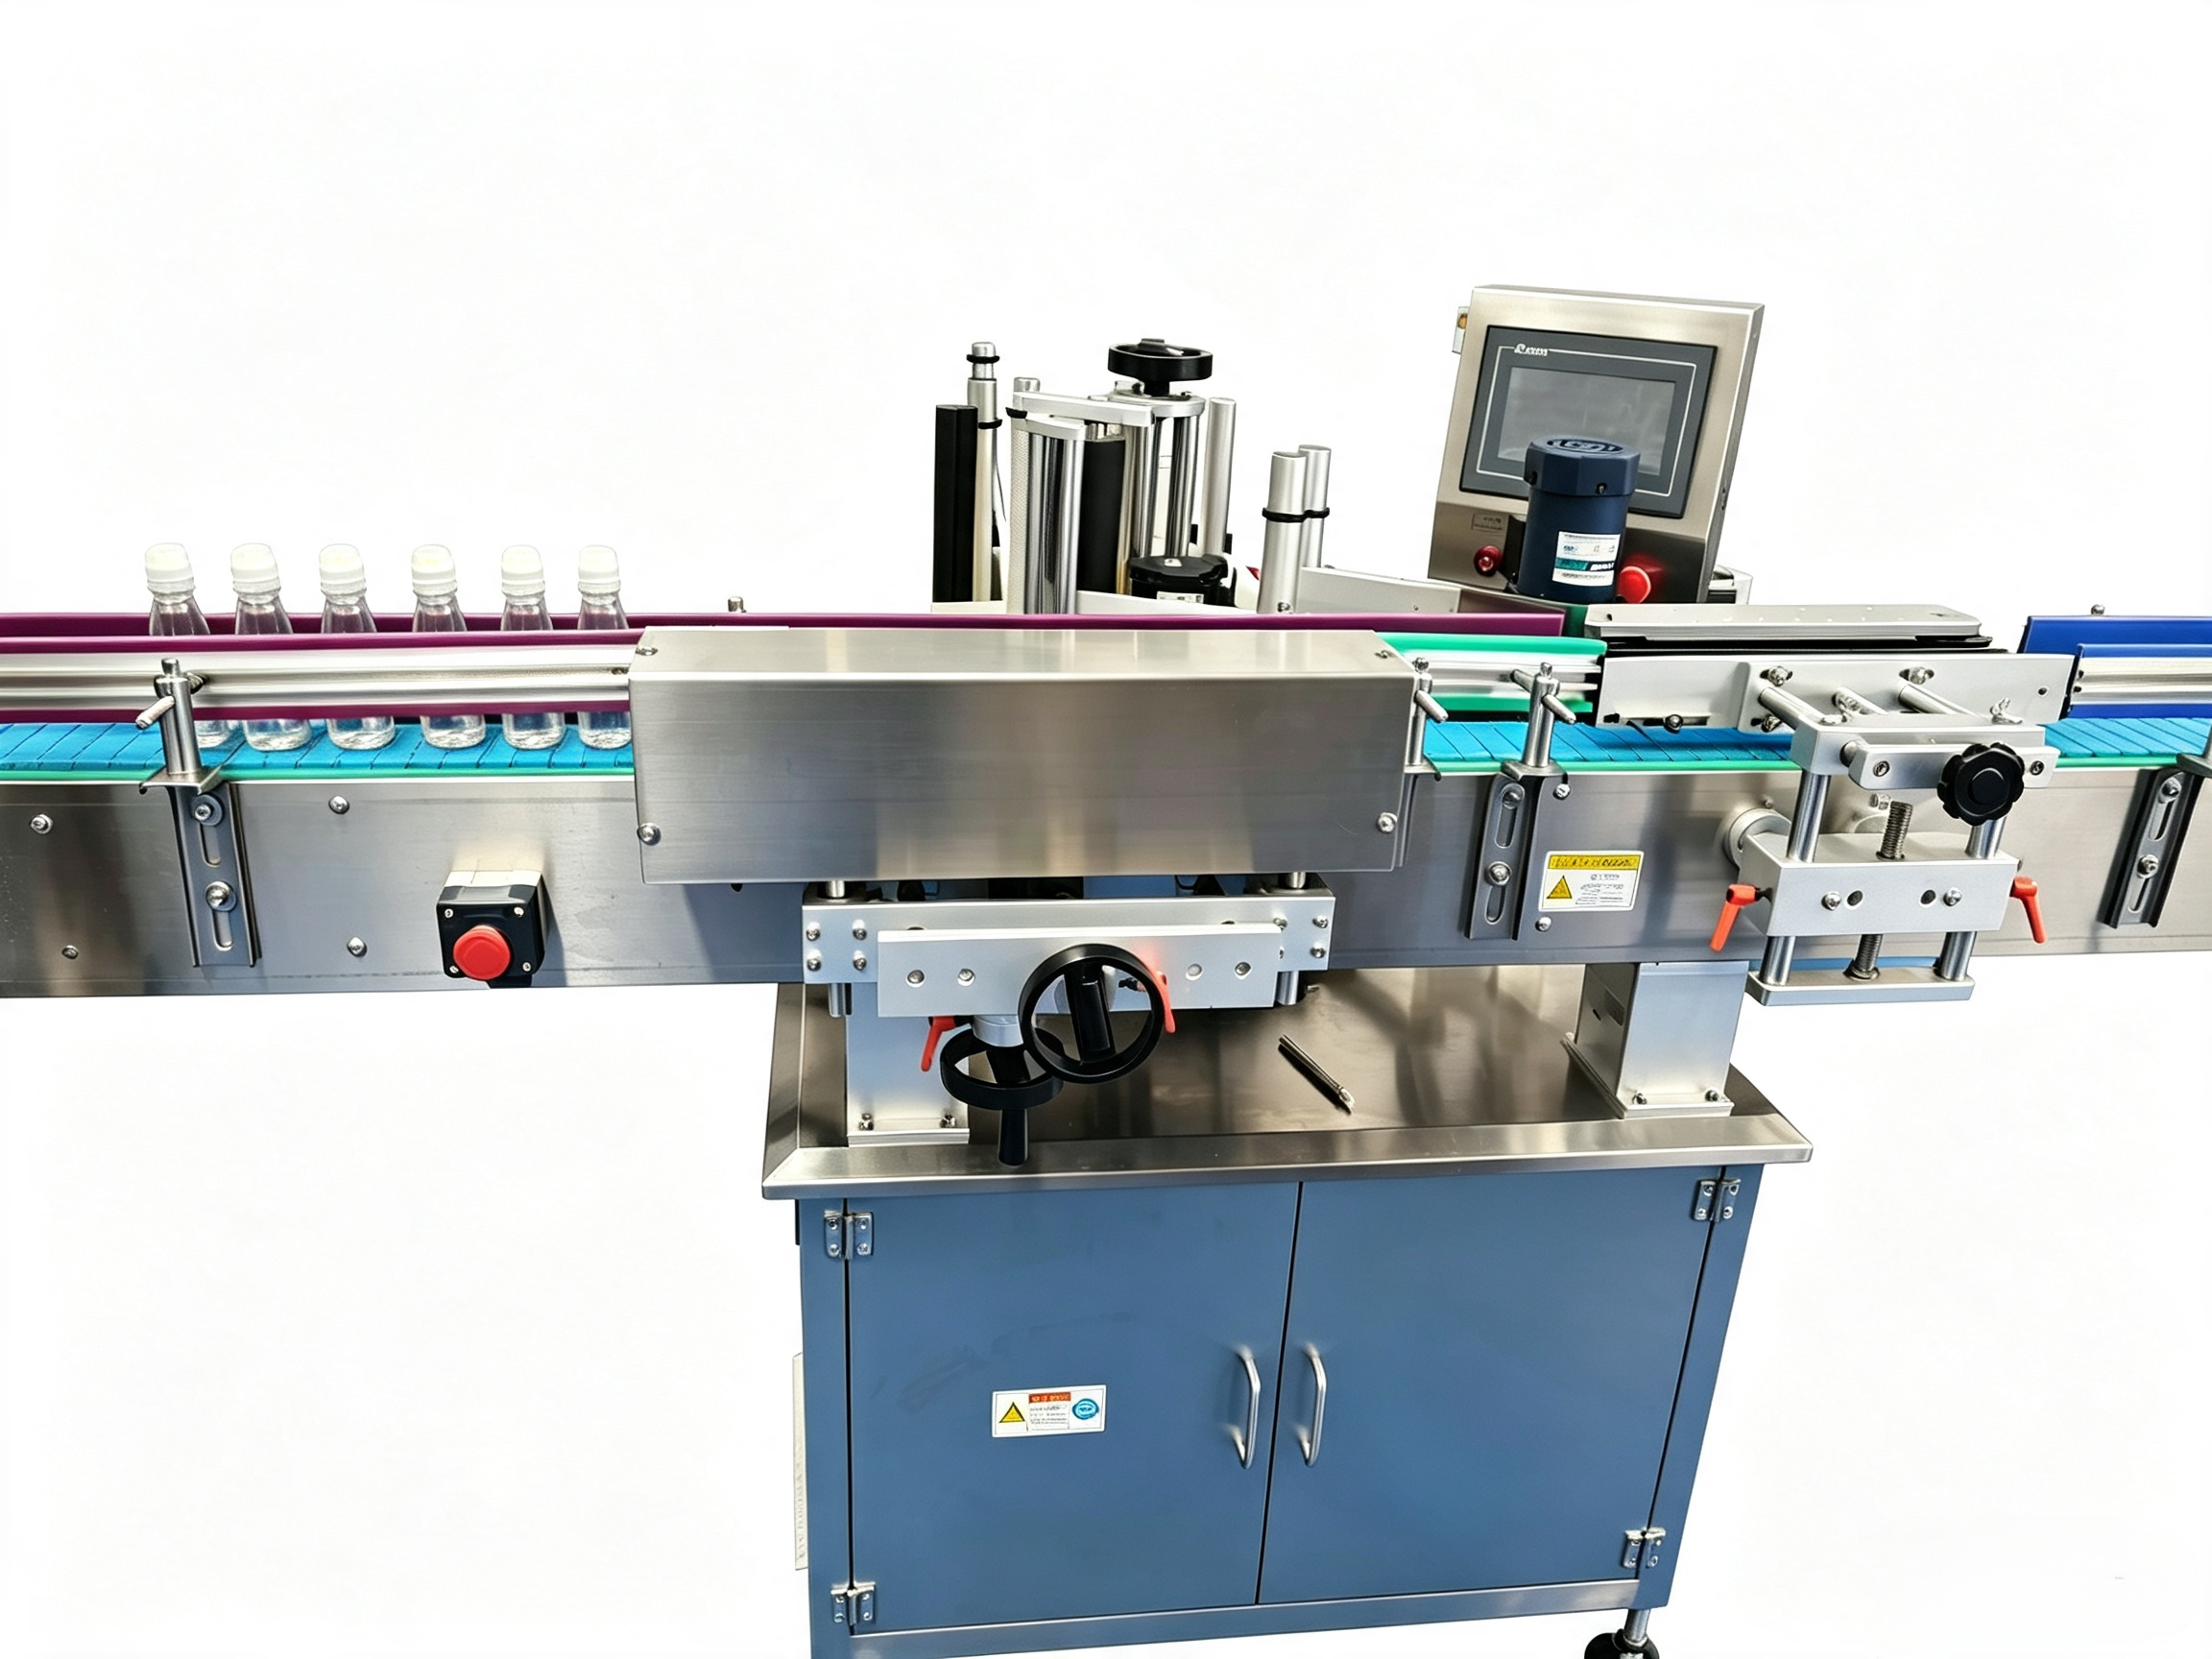
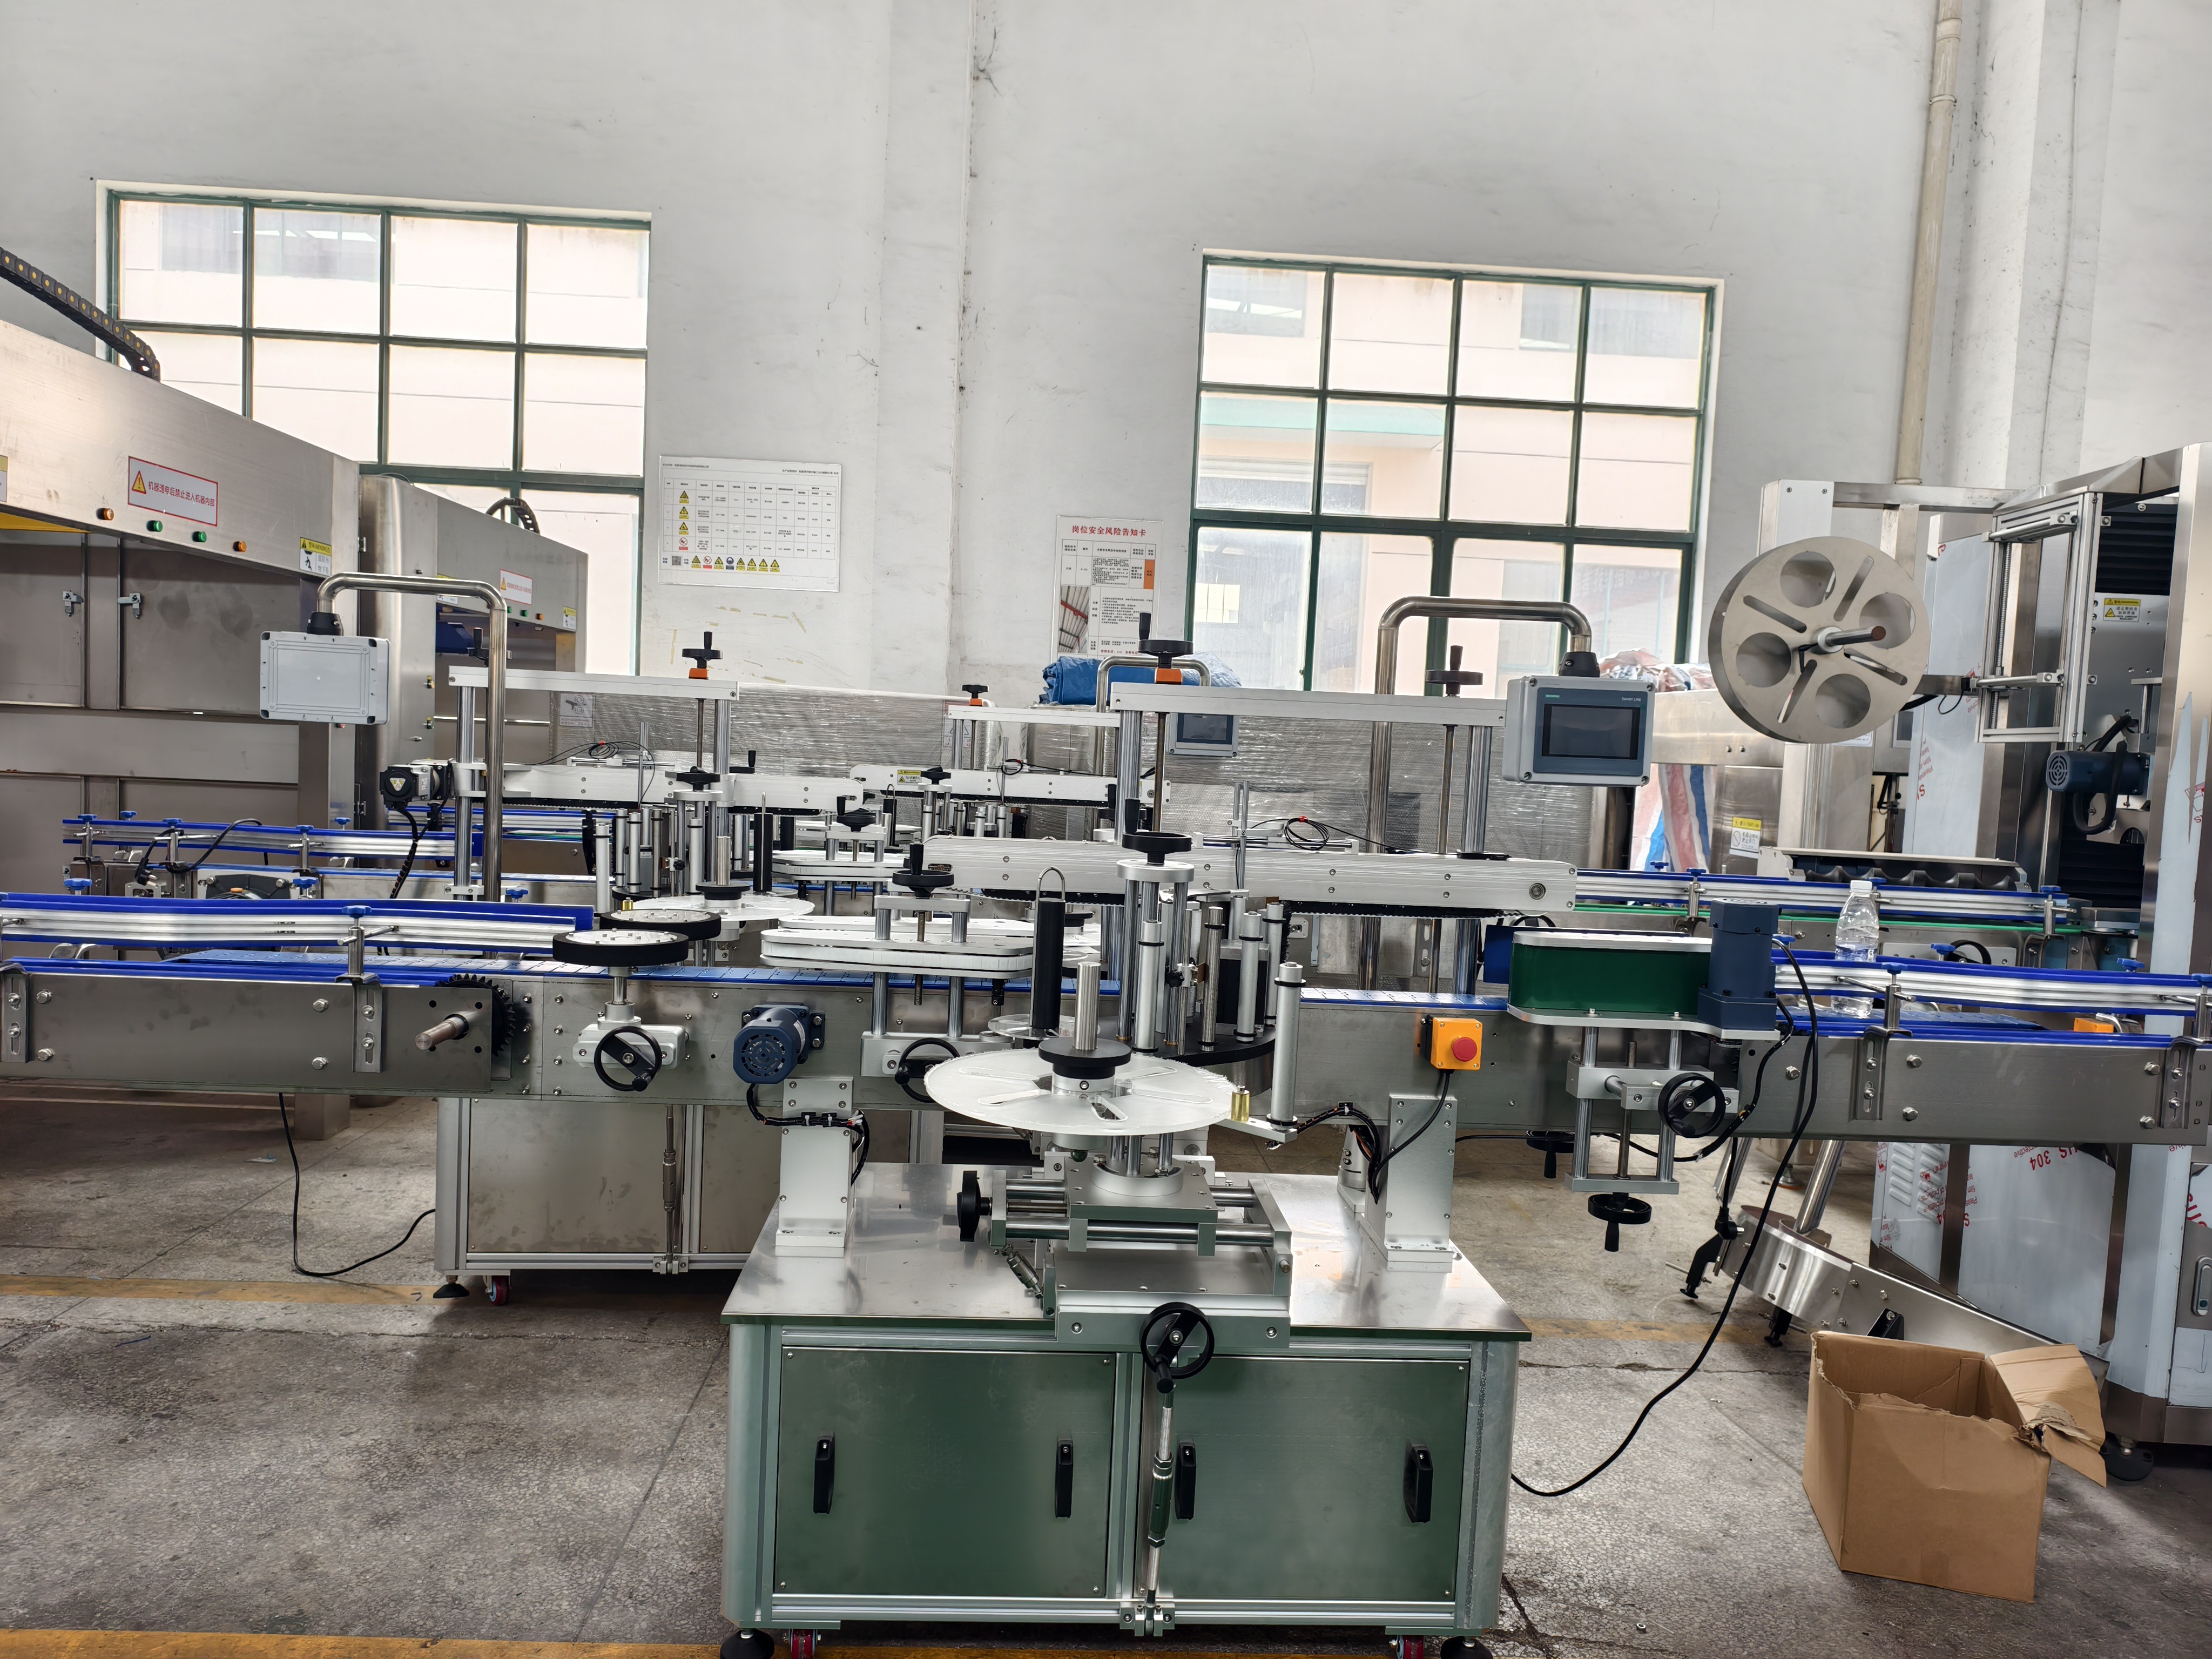
Sleeve and shrink labeling machine

Product Value
01
Full-body sleeving + Tamper-evidence/Anti-counterfeiting: Capable of applying full-body labels or neck bands with tamper-evident functionality.
02
Cost reduction and efficiency improvement: Replaces manual labeling.
03
Compatible with uniquely shaped bottles; enhances visual appeal and premium value.
04
Broad material compatibility: Supports mainstream heat-shrink films such as PVC, PETG, and OPS; keeps overall packaging costs under control.
Applicability boundaries

Containers
PET bottles, glass bottles, aluminum cans, plastic jars; preference for shapes that are roughly cylindrical, elliptical, or regularly shaped (non-standard).

Labels
PVC, PETG, or OPS heat-shrink sleeve film (typical thickness: 30–80 μm).
Working Principle
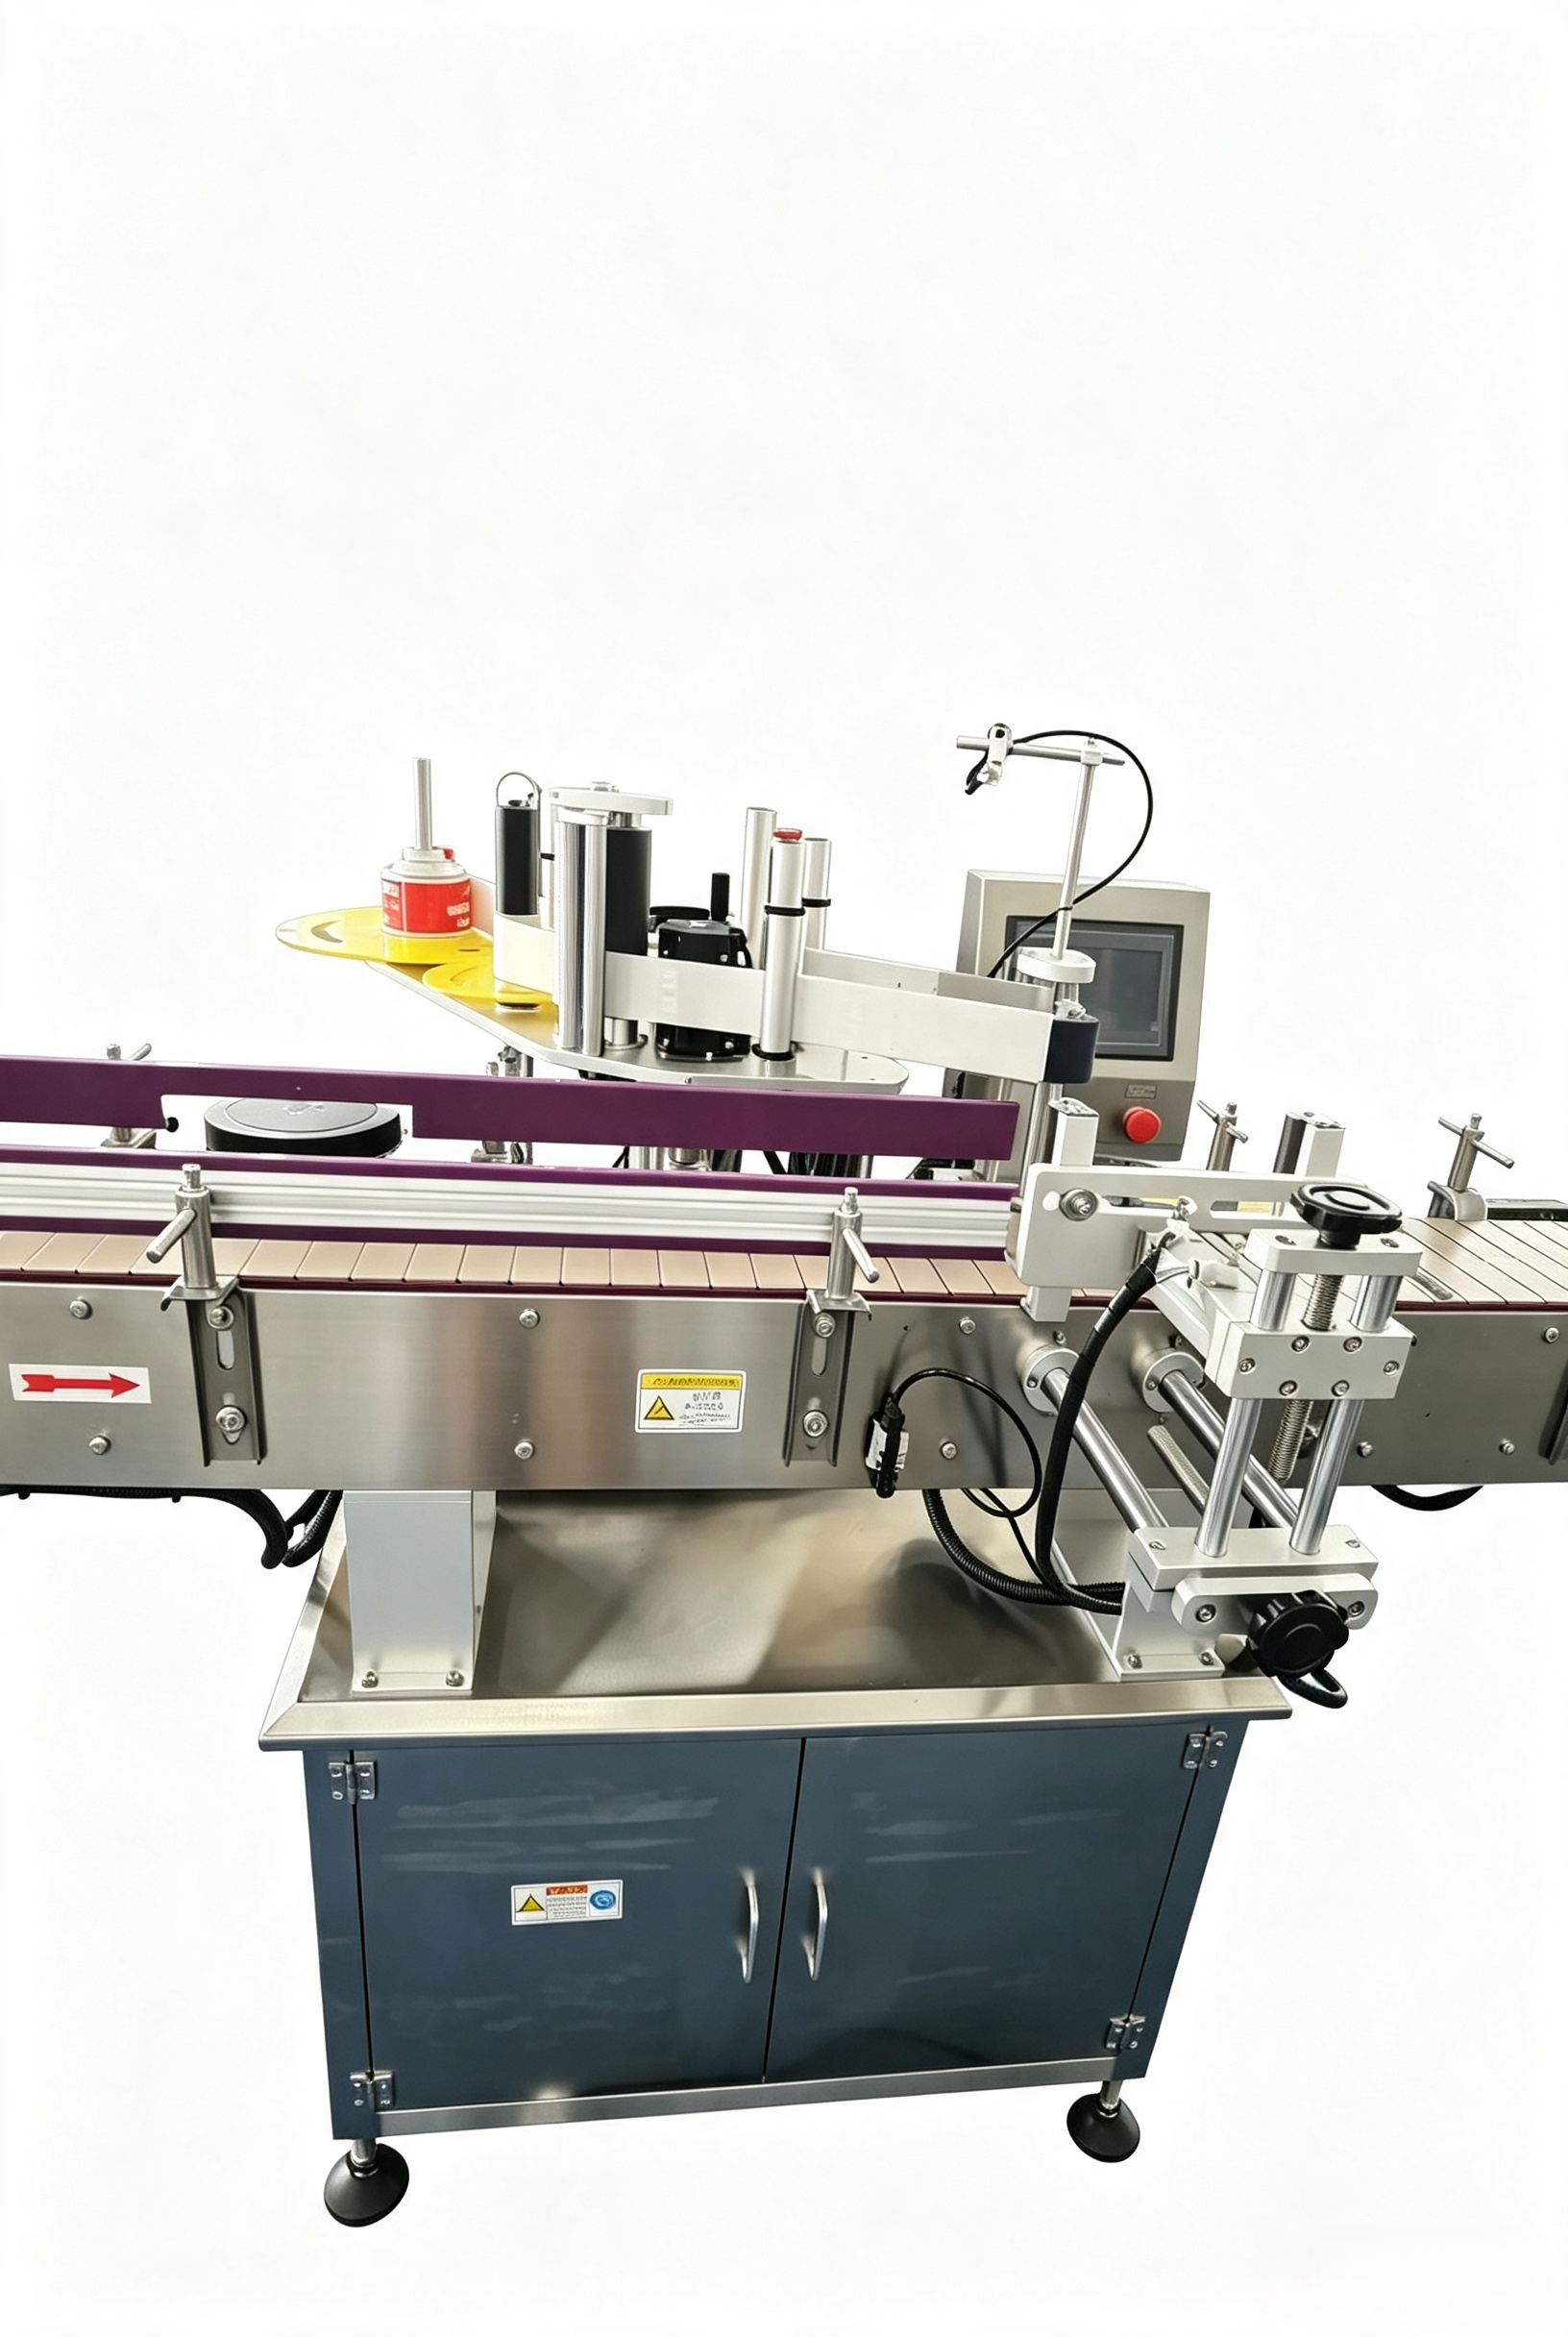
Constant-tension feeding of tubular film from a roll → cutting based on color mark registration → synchronous application onto the bottle body → heat tunnel processing (radial shrinkage of the tubular film to conform to and fit the bottle).
Core components
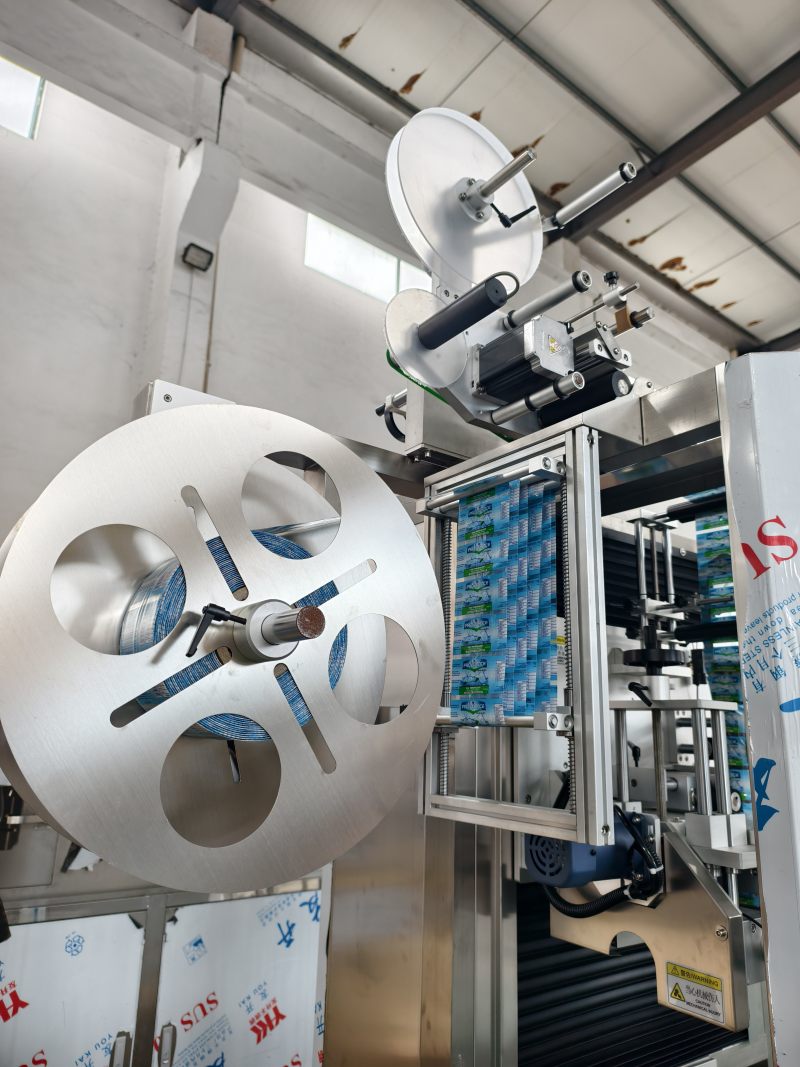
Unwinding Constant-Tension Mechanism
Film roll holder and tension damping/servo unwinding system; prevents film stretching, slackness, and label length inconsistencies.
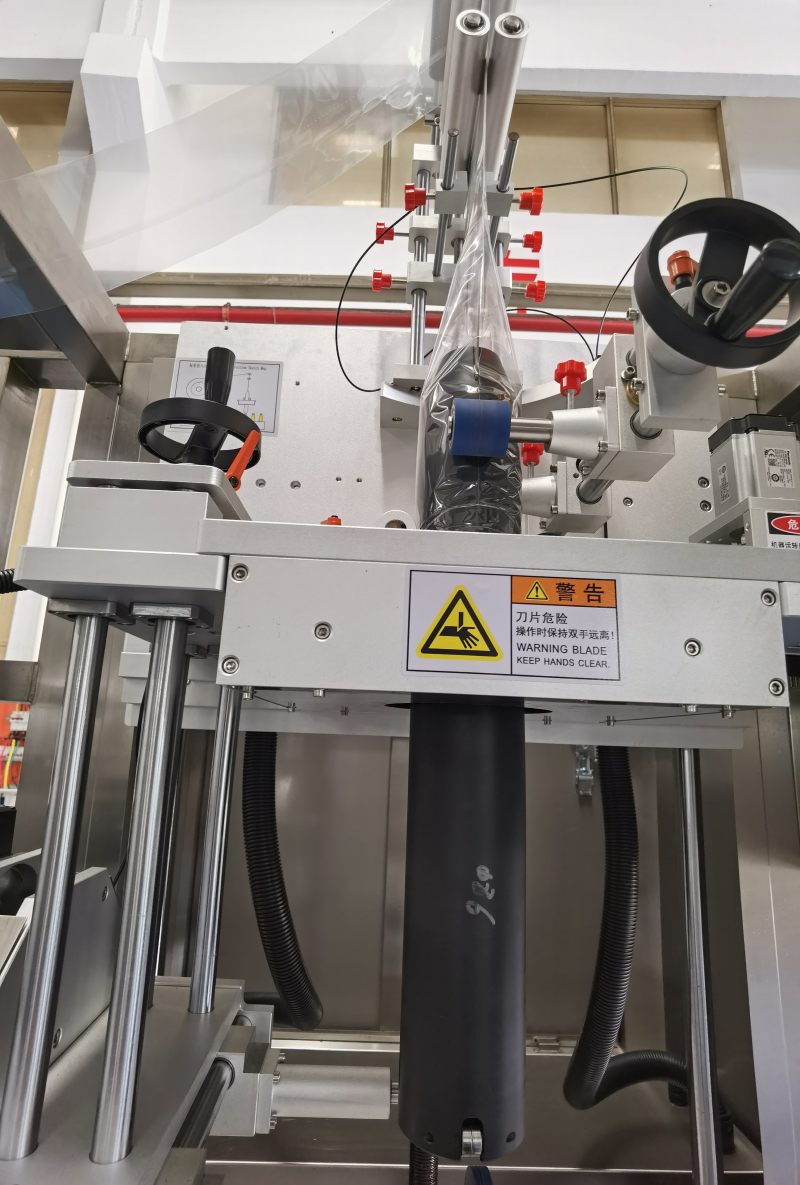
Film Feeding Servo + Film Guide Ring (Forming Tool)
Transforms flat film into a cylinder; determines concentricity and prevents film scratching.
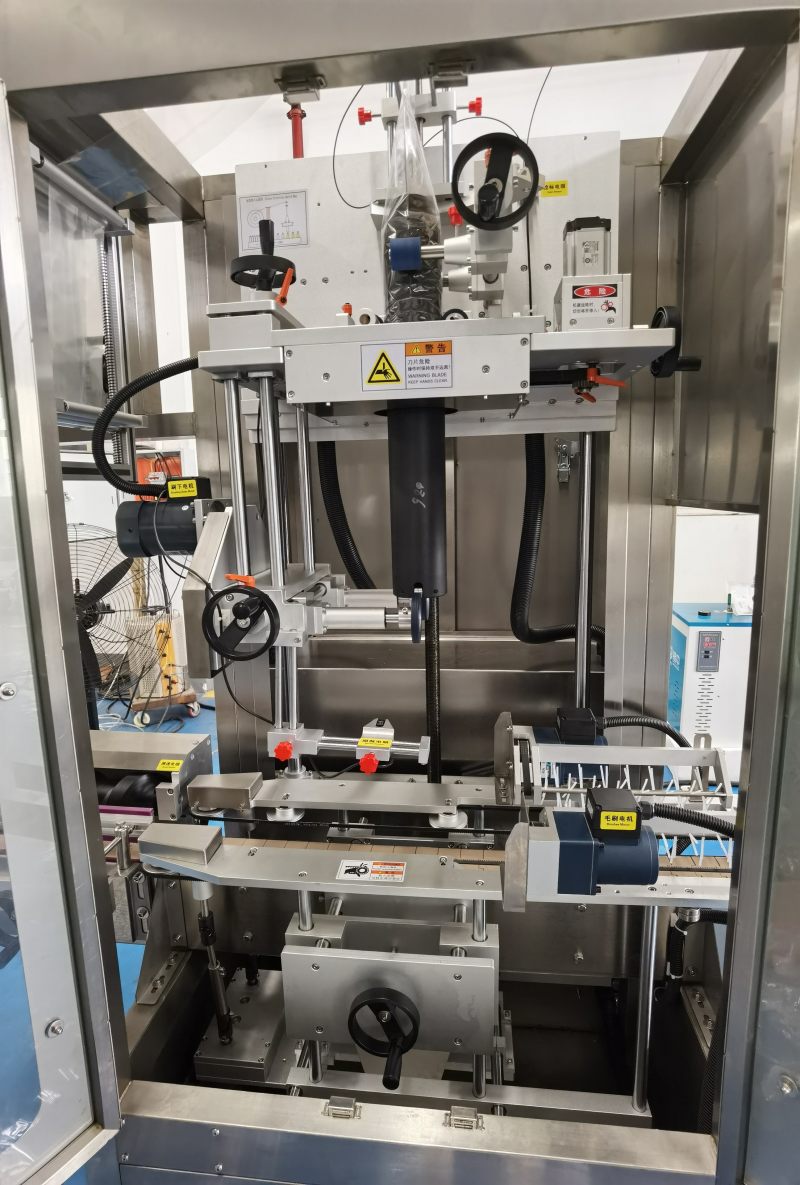
Registration Mark Sensor + Cutter Assembly
Rotary cutter or straight blade; controls label length and cutting precision; contains the most wear-prone components.
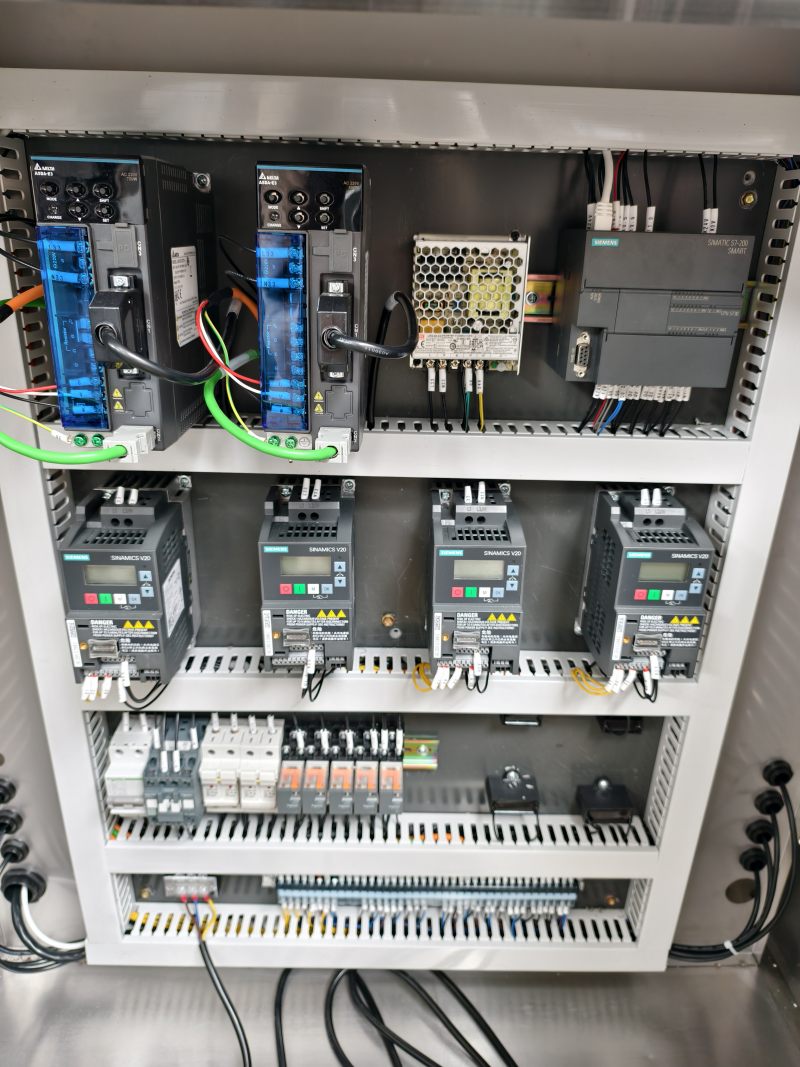
PLC + HMI + Main Servo
Manages system-wide timing synchronization, parameter storage, and one-touch format switching.
Optional
01
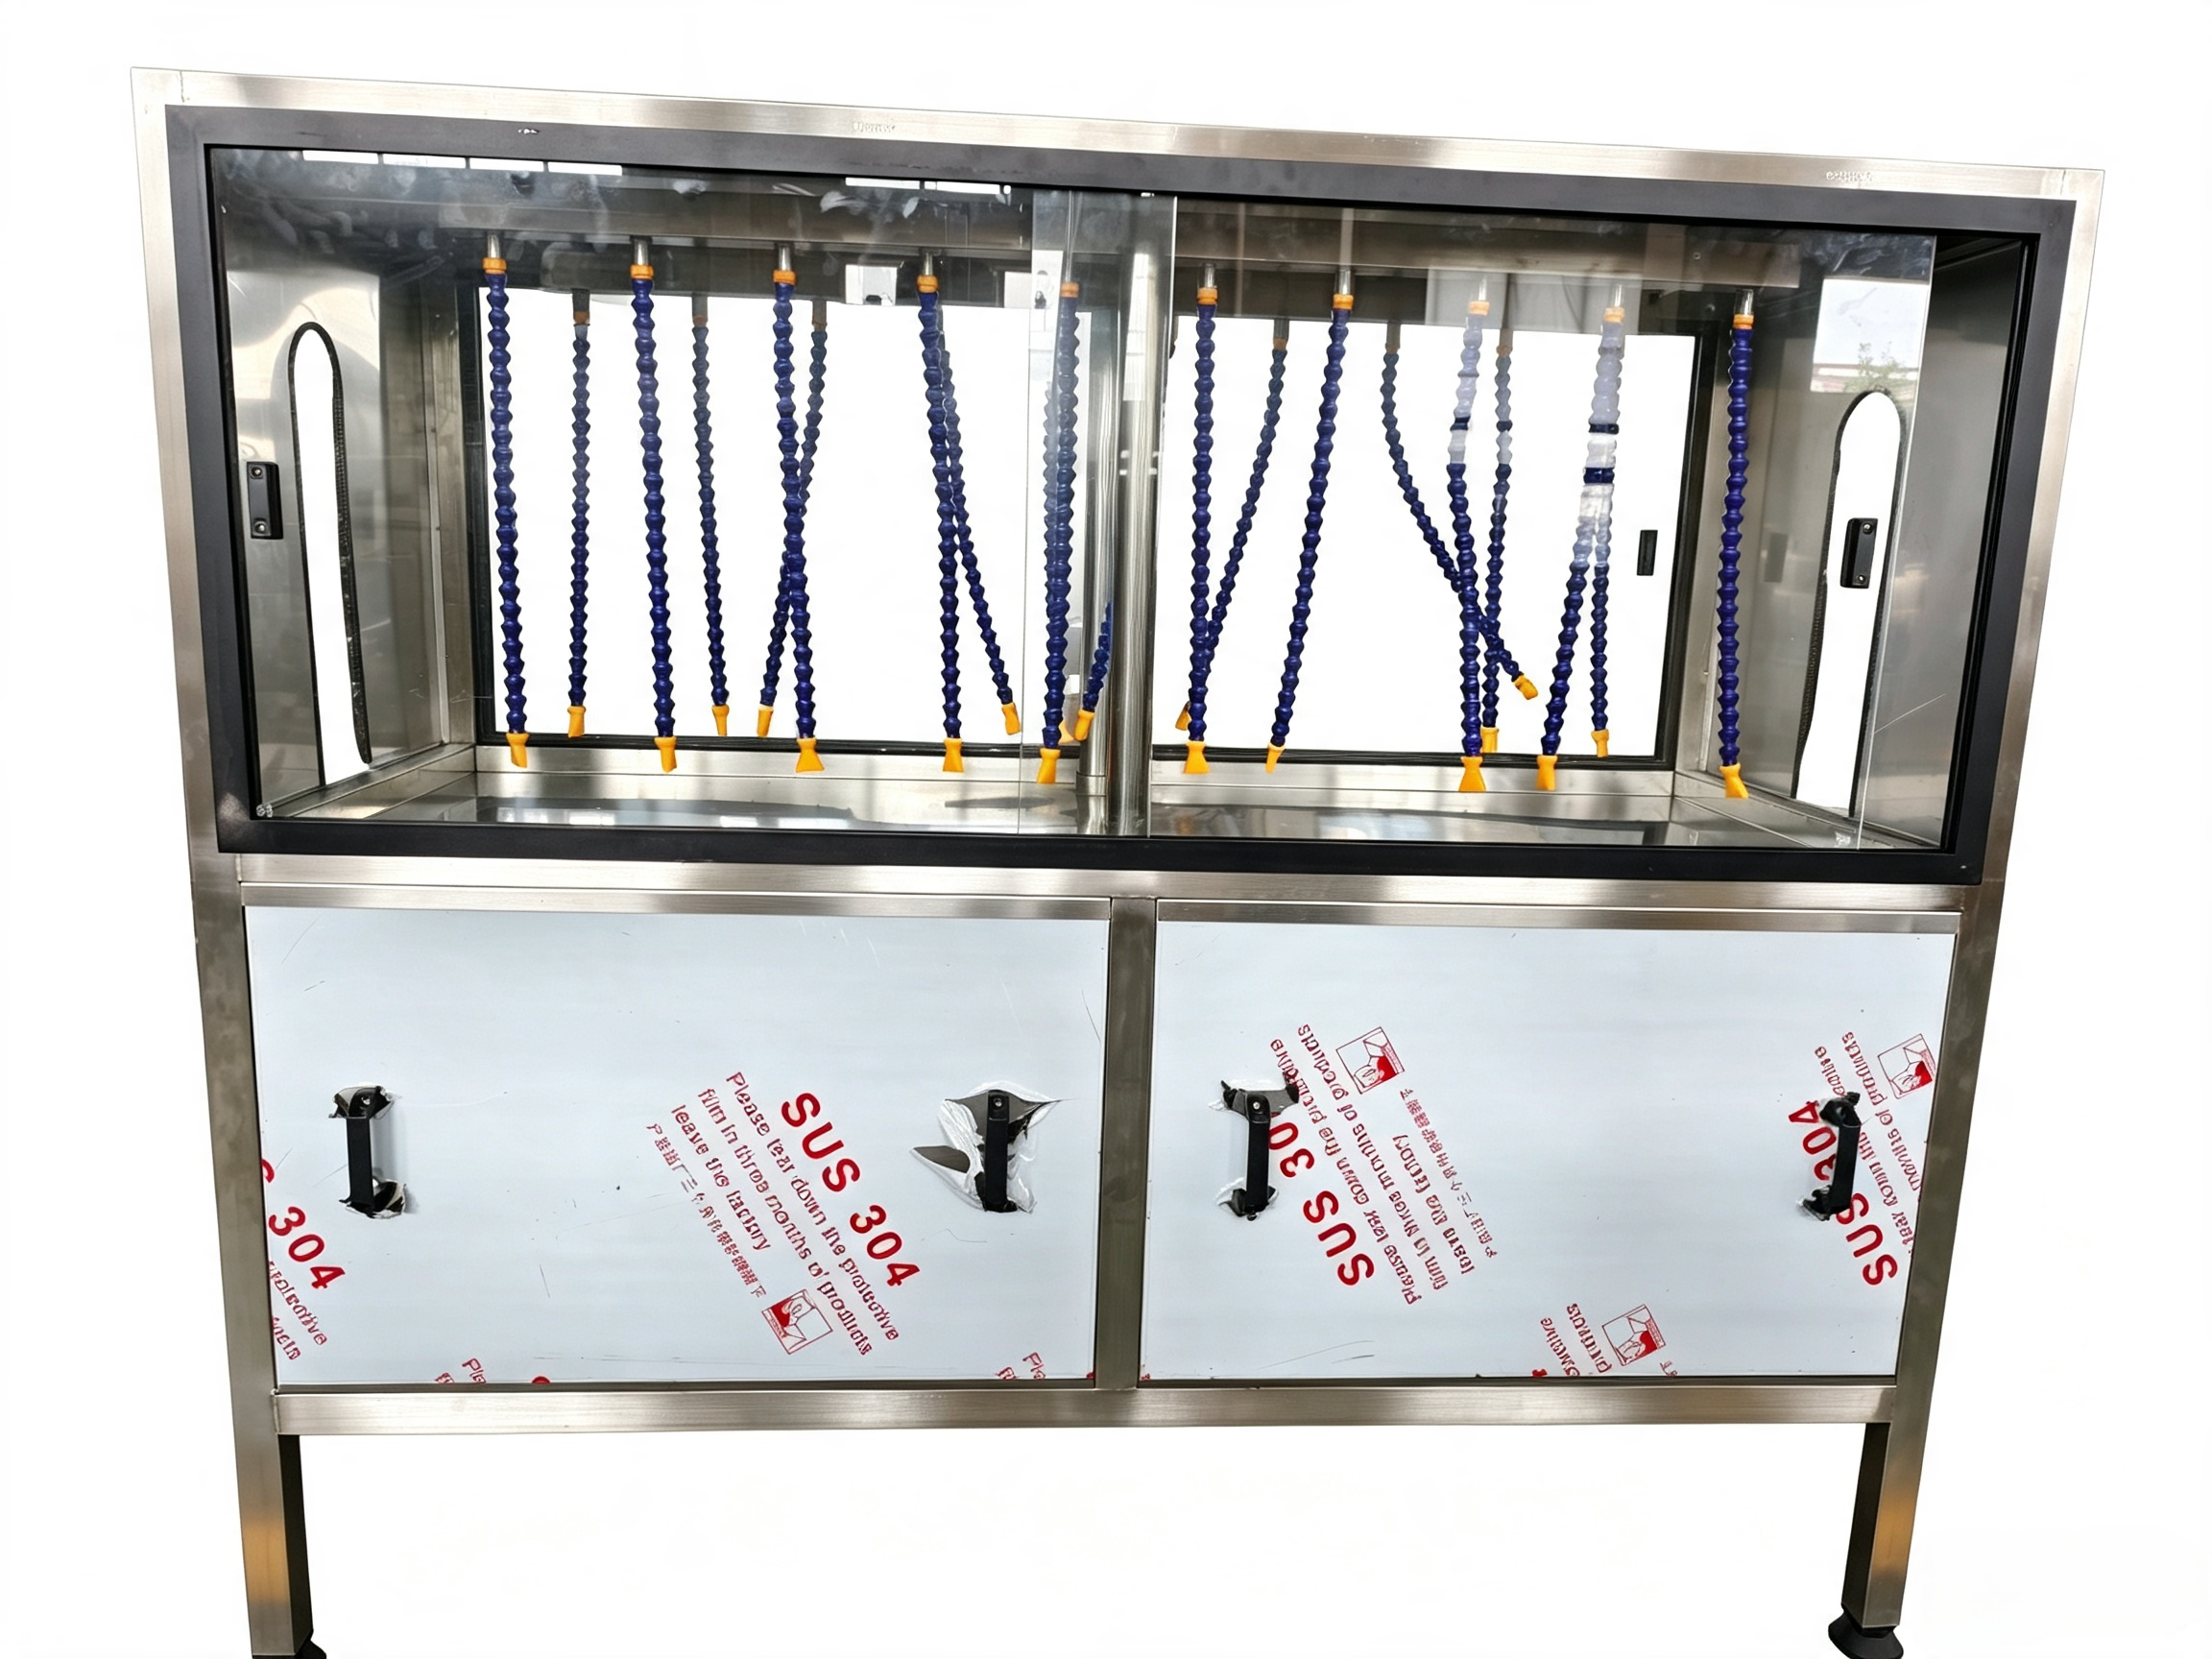
Steam generator (steam shrink oven, for more uniform shrinkage, suitable for PETG)
02
Hot air circulating shrink oven (no water vapor, suitable for products susceptible to condensation)
03
Quick changeover tooling, spare tool holder, spare forming device
Dual-head high-speed labeling module (doubles production capacity)
Changeover/Cleaning/Maintenance
Changeover
Engage safety lockouts; replace the forming tool, bottle-spacing screw, and positioning stops; load the recipe via the HMI and adjust label length, film feed, and oven temperature; perform a test run to calibrate concentricity and sleeve positioning, then save the parameters.
Maintenance
Daily checks on tension, cutting blades, photoelectric sensors, and oven temperature; weekly lubrication of guide rails and chains, plus inspection of cutters and forming tools for burrs; monthly inspection of timing belts and cleaning of dust from electrical controls; maintain a stock of wear parts such as blades, brushes, and film-guiding rings.
Why are the labels inconsistent in length, misaligned, or wrinkled?
Check these four points first: ① unstable tension; ② worn or misaligned forming tool; ③ dirty color-mark sensor or incorrect gain setting; ④ bottle instability during transport or unsynchronized bottle spacing.
How do I choose between a steam shrink tunnel and a hot-air shrink tunnel?
Steam → uniform shrinkage and high gloss, ideal for PETG; Hot-air → no moisture/condensation issues, ideal for cold-fill beverages, carbonated drinks, and moisture-sensitive products.
Can it be directly integrated with filling and blow-molding machines?
Yes. Standard models come equipped with interface signals and bottle infeed/outfeed connections, enabling synchronized line start/stop and automatic standby when bottles are missing.
How long does it take to switch bottle types?
For standardized quick-change models, switching between bottles in the same series takes 5–15 minutes; for significantly different shapes or large variations in bottle diameter, the forming tool and feed screw must be replaced, taking approximately 20–40 minutes.
Contact Us
Complete 2 easy steps below to get your factory matrix and a complimentary factory layout design within 24 hours.
Request Factory Price & Factory Layout Within 24h
Request Factory Price & Factory Layout Within 24h